Every product on a supermarket shelf has followed a carefully managed journey before reaching the customer. Fresh milk, packaged snacks, bottled drinks, frozen meals, and ready-to-eat foods all depend on controlled manufacturing conditions to maintain their quality. While consumers rarely think about what happens behind the scenes, food manufacturers know that even a slight variation in temperature, pressure, or humidity can affect the final product.
Maintaining consistent production has become more challenging as consumer expectations continue to rise. Businesses are expected to deliver safe, high-quality products while reducing waste and improving efficiency. This is why sensors for food & beverage industry operations have become an essential part of modern manufacturing. Rather than simply collecting data, these technologies help businesses make informed decisions that protect product quality from the beginning of production to final packaging.
Consistency Begins with Accurate Monitoring
Food manufacturing is built on precision. Every ingredient, every production stage, and every storage condition contributes to the quality customers expect. Whether processing dairy products, beverages, baked goods, or frozen foods, manufacturers rely on accurate measurements to keep production running smoothly.
Reliable monitoring allows production teams to identify small changes before they become larger problems. A minor increase in processing temperature or an unexpected pressure drop may seem insignificant at first, but over time these changes can affect product consistency, shelf life, and regulatory compliance.
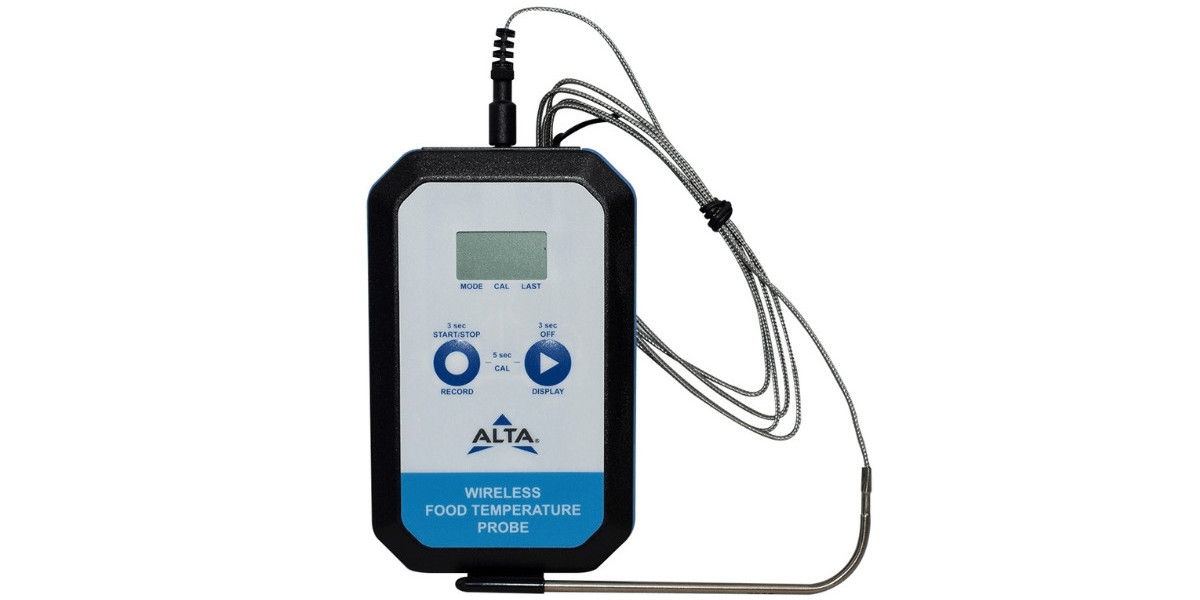
This is where sensors for food & beverage industry applications make a noticeable difference. They provide continuous information that helps manufacturers maintain stable production conditions while reducing the need for manual checks throughout the day.
Better Decisions Come from Better Data
Modern manufacturing is no longer based on assumptions. Production managers need reliable information that reflects what is happening throughout the facility in real time. Accurate data allows teams to respond quickly, improve efficiency, and prevent unnecessary downtime.
When sensors continuously monitor equipment and production environments, businesses gain greater visibility into their operations. Instead of reacting after problems appear, manufacturers can identify patterns that support preventative maintenance and smarter production planning.
This shift toward data-driven decision-making has helped many food manufacturers reduce waste while improving the consistency customers have come to expect.
Automation Supports People, Not Just Production
Technology is sometimes viewed as a replacement for manual work, but successful automation serves a different purpose. Its greatest value comes from allowing employees to spend less time responding to routine issues and more time focusing on quality improvement.
Modern process controllers for industry work alongside monitoring equipment to maintain stable operating conditions throughout production. When measurements begin moving outside acceptable limits, these controllers can automatically adjust equipment without waiting for manual intervention.
The result is a smoother production process where operators remain in control while repetitive adjustments happen automatically. This balance allows experienced teams to focus on product quality instead of constantly monitoring individual machines.
Maintaining Food Safety Every Day
Food safety depends on consistency rather than occasional inspection. Every production shift must follow carefully controlled conditions to ensure products remain safe for consumers.
Temperature plays a critical role in cooking, cooling, storage, and transportation. Moisture levels influence product freshness, while pressure and flow affect manufacturing performance across many production lines. Monitoring these conditions continuously helps reduce the likelihood of contamination or product spoilage.
Reliable sensors for food & beverage industry solutions support these requirements by providing accurate measurements throughout the manufacturing process. Instead of relying only on scheduled inspections, businesses gain continuous oversight that strengthens both quality assurance and regulatory compliance.
Supporting Long-Term Operational Efficiency
Every manufacturing facility looks for ways to improve productivity without sacrificing product quality. While large investments often attract attention, meaningful improvements frequently come from smaller operational changes that deliver long-term value.
Continuous monitoring helps manufacturers identify equipment that requires maintenance before unexpected failures occur. Small performance changes often appear in sensor readings long before machines stop operating completely. Early detection reduces costly downtime while extending equipment life.
At the same time, process controllers for industry help maintain consistent production settings across multiple manufacturing stages. Stable operating conditions reduce unnecessary product variation and improve resource efficiency throughout the facility.
Rather than increasing complexity, these systems simplify everyday operations by helping production teams work with greater confidence.
Building Consumer Trust Through Consistent Quality
Consumers expect every product they purchase to meet the same standard every time. Whether buying a favourite beverage or a packaged food product, consistency influences purchasing decisions just as much as taste or appearance.
Manufacturers earn that trust by maintaining reliable production processes behind the scenes. Accurate monitoring ensures recipes remain consistent, storage conditions stay within acceptable limits, and production equipment continues operating efficiently.
By using dependable sensors for food & beverage industry technologies, manufacturers strengthen quality control while protecting the reputation they have built with customers over many years.
Preparing Manufacturing for the Future
The food and beverage industry continues to evolve as businesses embrace smarter manufacturing technologies. Digital monitoring, connected equipment, and predictive maintenance are becoming valuable tools for organisations seeking greater efficiency without compromising food safety.
Future production facilities will increasingly rely on connected monitoring systems that provide instant visibility across every stage of manufacturing. Combined with advanced process controllers for industry, these technologies will help manufacturers make faster decisions while reducing energy consumption, production waste, and maintenance costs.
Although technology continues to improve, its purpose remains the same. It exists to support better products, stronger quality standards, and more efficient manufacturing processes that benefit both businesses and consumers.
Moving Forward with Confidence
Successful food manufacturing is built on thousands of small decisions made every day. Maintaining consistent temperatures, monitoring production conditions, and responding quickly to changing environments all contribute to the quality consumers expect. Reliable monitoring technology allows businesses to protect product integrity while improving efficiency across every stage of production.
As manufacturing continues to become more connected, investing in dependable sensors for food & beverage industry solutions and advanced process controllers for industry provides a practical foundation for long-term growth. These technologies help create safer workplaces, stronger quality control systems, and more reliable production outcomes without losing sight of the people responsible for delivering exceptional products.
Businesses looking to strengthen their monitoring capabilities with trusted industrial instrumentation and expert technical support can explore the comprehensive solutions available through OneTemp, helping manufacturers build smarter, safer, and more efficient food and beverage operations.